

Cut plates
Using our extensive cutting capacities (plasma, laser, water jet and sawing), we can guarantee our clients high quality products with tight tolerances and delivered in a fast and reliable time frame delivery.
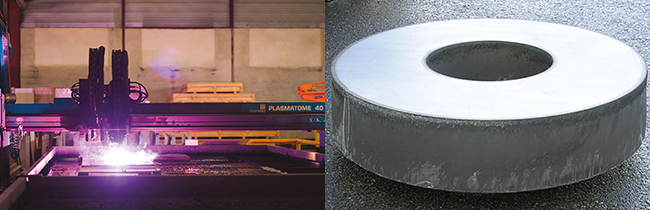
The most economical solution for all forms of stainless steel and nickel alloy pieces.
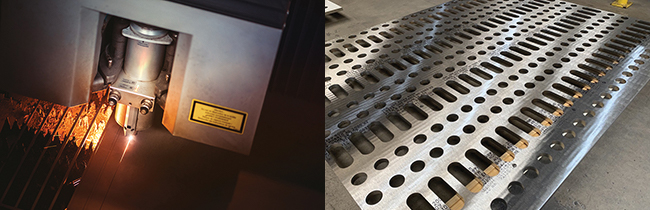
The high precision of the laser allows tight tolerances up to 50mm thickness. Also ideal for large quantities of pieces.
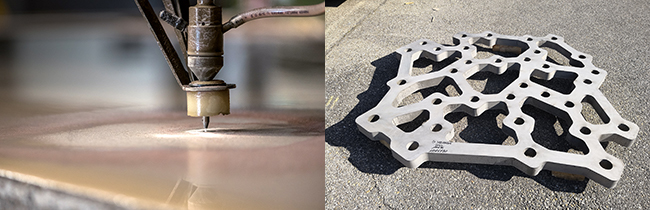
High-pressure water jet cutting reduces or avoids possible machining. No shape or thickness limitations, cold cutting without heat affected zone (HAZ). Ideal for complex cutting of stainless steels and nickel alloys.
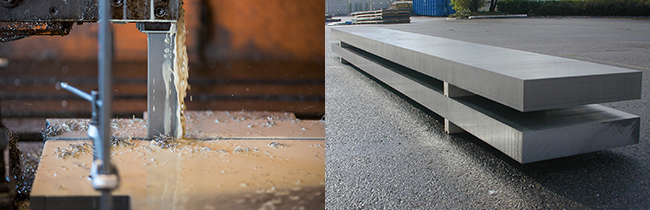
Sawing ensures a good cutting perpendicularity for medium and thick pieces and flats, without a heat affected zone (HAZ).
Compare tolerances according their cutting processes
| Plate thickness (mm) | SAW | |
|---|---|---|
| L ≤ 3000 mm | L > 3000 mm | |
| 1 → 5 | Length 0 / + 4 mm Width 0 / + 4 mm |
Length 0 / + 6 mm Width 0 / + 4 mm |
| 6 → 10 | ||
| 11 → 15 | ||
| 16 → 20 | ||
| 21 → 30 | ||
| 31 → 40 | ||
| 41 → 50 | ||
| 51 → 60 | ||
| 61 → 80 | ||
| 81 → 100 | ||
| 101 → 110 | ||
| 111 → 130 | ||
| 131 → 139 | ||
| 140 → 150 | ||
| – | ||
| Plate thickness (mm) |
LASER | ||
|---|---|---|---|
| L ≤ 300 mm | L > 300 mm
L ≤ 1000 mm |
L > 1000 mm | |
| 1 → 5 | ± 0,3 mm | ± 0,5 mm | ± 0,6 mm |
| 6 → 10 | |||
| 11 → 15 | ± 0,75 mm | ± 1 mm | ± 1,25 mm |
| 16 → 20 | |||
| 21 → 30 | ± 1 mm | ± 1,25 mm | ± 1,5 mm |
| 31 → 40 | ± 2,5 mm | ± 3 mm | ± 3,5 mm |
| 41 → 50 | |||
| 51 → 60 | N.A. | ||
| 61 → 80 | |||
| 81 → 100 | |||
| 101 → 110 | |||
| 111 → 130 | |||
| 131 → 139 | |||
| 140 → 150 | |||
| ■ Minimum hole diameter: 0,4 x thickness | |||
| Plate thickness (mm) |
WATERJET | |||||
|---|---|---|---|---|---|---|
| L ≤ 1000 mm | L > 1000 L ≤ 3000 |
L > 3000 L ≤ 6000 |
||||
| Basic | Normal | Fine | ||||
| 1 → 5 | ± 0,8 mm | ± 0,6 mm | ± 0,4 mm | ± 2 mm | ± 3 mm | |
| 6 → 10 | ± 1 mm | ± 0,7 mm | ± 0,4 mm | |||
| 11 → 15 | ||||||
| 16 → 20 | ± 1,5 mm | ± 1 mm | ± 0,5 mm | |||
| 21 → 30 | ||||||
| 31 → 40 | ||||||
| 41 → 50 | ± 2 mm | ± 1,5 mm | ± 1 mm | ± 2,5 mm | ± 3,5 mm | |
| 51 → 60 | ||||||
| 61 → 80 | ||||||
| 81 → 100 | N.A. | ± 2,5 mm | ± 1,5 mm | ± 3,5 mm | ± 4,5 mm | |
| 101 → 110 | N.A. | ± 3,5 mm | ± 2,5 mm | ± 4,5 mm | ± 5,5 mm | |
| 111 → 130 | ||||||
| 131 → 139 | N.A. | ± 5 mm | ± 4 mm | ± 6 mm | ± 7 mm | |
| 140 → 150 | ||||||
| ■ Taper included (0,2 mm per each 10 mm thick)
■ Minimum hole diameter: 0,4 x thickness |
||||||
| Plate thickness (mm) |
PLASMA | |||||
|---|---|---|---|---|---|---|
| Upper surface without taper Δ |
Potential taper □ |
Minimum overlength rough size versus finished size ◊ |
||||
| 1 → 5 | External cut 0 / + 3 mm Internal cut -3 / 0 mm |
3 mm per side / Total 6 mm |
5 mm per side : + 10 mm total |
|||
| 6 → 10 | ||||||
| 11 → 15 | ||||||
| 16 → 20 | ||||||
| 21 → 30 | ||||||
| 31 → 40 | ||||||
| 41 → 50 | ||||||
| 51 → 60 | ||||||
| 61 → 80 | External cut 0 / + 5 mm Internal cut – 5 mm / 0 |
6 mm per side / Total 12 mm |
< 80 mm → 6 mm per side : + 12 mm total |
|||
| 81 → 100 | < 100 mm → 7 mm par côté : + 14 mm total |
|||||
| 101 → 110 | ≤ 110 mm → 10 mm par côté : + 20 mm total |
|||||
| 111 → 130 | External cut 0 / + 8 mm Internal cut – 8 mm / 0 |
External cut 10 mm per side / Total 20 mm. |
< 140 mm → 12 mm per side + 24 mm total |
|||
| 131 → 139 | ||||||
| 140 → 150 | ≥ 140 mm → 15 mm per side : + 30 mm total |
|||||
| Δ That which can be measured with a measuring tape, on surface
□ Could be partially negative above thickness 100 mm ◊ Rough size (theoretical cut), finished size (machined): Necessary for the client to eliminate the HAZ and the irregular taper As a precaution, always inform the finished sizes for thickness above 100 mm ■ Minimum hole diameter: 1,5 x thickness (always ≥ 20 mm) ■ Minimum ring wall: 0,5 x thickness (always ≥ 30 mm) |
||||||
Général
- No flatness or straightness guarantee on cut pieces, unless prior agreement
- Flatness tolerances according standards, only apply to full plates
- Hot rolled plate thickness tolerances: ASTM A480 & ISO 18286
- Surface according to EN 10163-2 class B3 (Scratches, grinded areas)
- Cut edges, deburred
- By default, handwritten felt-tip marking “Grade, heat number”. Laser marking when laser cut